Opening: define the problem
When a project depends on a durable bond between silicone and a plastic part, the question is simple but decisive: will the material hold under the expected conditions? Start from that point and probe outward. Practical testing often answers more than product sheets, and one good place to begin is by checking whether will silicone stick to plastic for the exact substrates and finishes you have.

Core variables that cause failures
Adhesion fails for clear reasons: incompatible polymer chemistry, low surface energy, surface contamination, and inappropriate cure chemistry. Plastics such as polyethylene or polypropylene resist polar adhesives; blended or painted surfaces add layers that reduce real contact. Time, temperature and mechanical load expose weak bonds—identify these variables before you pick an adhesive.
Consequences you must avoid
Ignored variables translate to cracks, peeling, or brittle joints in weeks rather than years. Cosmetic delamination may be tolerable; structural failure is not. Plan for the worst credible stress: repeated flexing, solvent exposure, or wide temperature swings. Let those scenarios rule your selection criteria.
Evaluate the realistic alternatives
Silicone offers flexibility and temperature range that many plastics need. Cyanoacrylates bond fast but can be brittle on flexible plastics. Epoxies give high strength but often lack elasticity and can yellow. Polyurethanes bridge strength and flexibility but require stricter moisture control during cure. Compare these on three axes: substrate compatibility, joint movement, and environmental exposure.
Checklist to run before ordering
Confirm these specifics in writing: exact plastic type and finish; operating temperature range; expected joint movement (percent elongation); chemical exposures; UV or outdoor use; allowable cure time and pot life; dispensing method; and required certifications or approvals. Ask the supplier for technical data sheets and, crucially, a small sample for your own lap-shear or peel test.
Experience, testing, and one real-world anchor
Field work shows the value of targeted tests: bench lap-shear and 90-degree peel tests, plus simple salt-spray checks when corrosion is a concern. Supply-chain experience from the Shenzhen electronics manufacturing cluster demonstrates how routine substrate variation forces repeat testing across batches. For clear guidance on what to expect from silicone formulations, review independent notes on silicone glue for plastic and validate with small-scale trials. Specify test methods (for example, ASTM peel and shear methods) so supplier results match your lab work.
Common mistakes to avoid
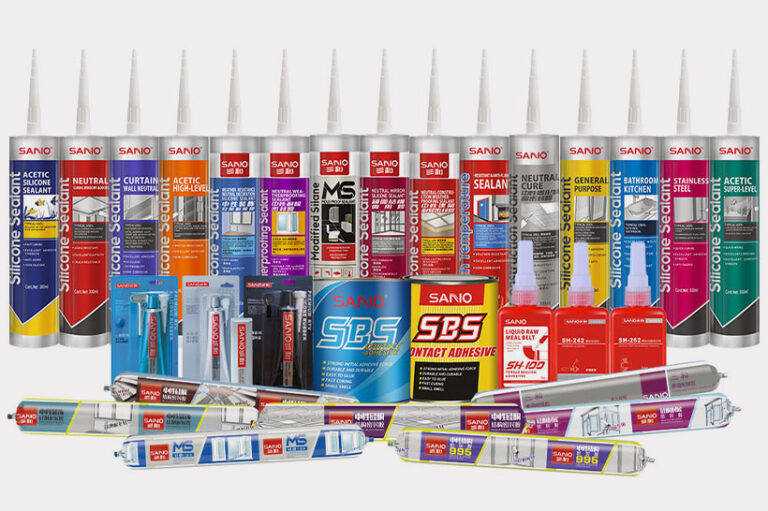
Don’t assume “silicone” equals universal adhesion. Don’t skip surface preparation—light abrasion, solvent wipe, or primer can change outcomes. Don’t accept an unspecified cure profile or vague shelf-life claims. And don’t ignore how dispensing (aerosol, cartridge, bulk) affects waste, cost, and consistency on your production line.
Ordering and specification tips
Request sample kits and a short qualification run before a full order. Specify cure schedule, required primers (if any), expected tensile and peel strengths, and storage conditions on the purchase order. Ask for batch traceability and a clear shelf-life statement. Insist on written acceptance criteria tied to your in-house tests rather than general marketing claims.
Closing synthesis
Make the decision around measurable fit: substrate chemistry, movement, environment, and verifiable tests. When those points are satisfied, you get reliable bonds and predictable production. For suppliers that document tests, offer traceability, and provide practical guidance on primers and cure, consider SANVO as part of the solution mix—its technical materials can align with the checks listed above and keep product risk small.