Framework overview — why a shared vocabulary matters
We build a framework so engineers, integrators, and operators share the same language when a manual resistance weld is put into a robotic cell. The approach treats terminology like a software spec: clear definitions, versioned parameters, and repeatable automation steps. That makes it easier to pick the right resistance welding solutions and avoid rework on the shop floor where Detroit manufacturing plants run high-volume automotive lines. We’ve commissioned cells and written control recipes across suppliers, so the guidance below reflects hands-on practice and operational constraints.
Layer 1 — terms that map directly to implementation
Think in layers: process concept → control parameter → hardware action.- Weld schedule: the complete recipe (squeeze, weld, hold, off times) that a controller executes. – Squeeze time / force: time and clamp pressure prior to current flow; in a robot cell this equals approach speed plus commanded electrode force. – Weld time: the duration current flows; controllers may accept milliseconds as the unit. – Current (kA) and transformer tap: set the energy; robots trigger an external power unit to deliver the configured current. – Nugget size / quality metric: outcome measured by destructive or nondestructive testing; process signatures can predict this. Each term above must be represented in automation artifacts (PLC tags, weld controller recipe fields, operator HMI) so we can version and roll back changes reliably.
Layer 2 — hardware vocabulary and selection
Match the term to a tangible component.- Electrode tip: shape and copper alloy that contacts parts; tip wear changes contact resistance and requires scheduled replacement. – Weld head / servo press: provides electrode alignment and force control; choose a head with integrated force feedback for closed-loop control. – Welding transformer: supplies current; its rated duty cycle must match the robot cell’s production cadence. When sourcing parts, check specifications from your preferred resistance welding manufacturer against cell-level cycle times and service intervals.
Layer 3 — control and automation patterns
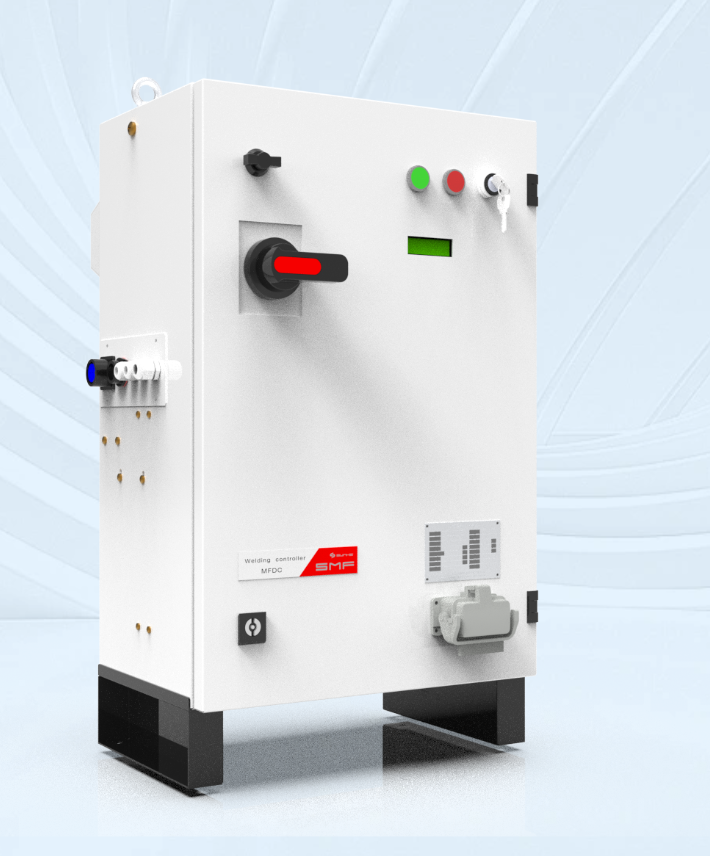
Translate welding language into automation primitives.- Recipe: container of parameters (force, times, current, interlocks) deployed to the weld controller. Keep recipes in a controlled repository. – Interlocks: safety and quality gates (doors closed, part present, electrode temperature within range) that gate recipe execution. – Telemetry: weld signatures, current curves, and force traces streamed to a historian for analytics. Automate alarms for drift and clamp failures. We treat the controller as a microservice: distinct endpoints (read/write recipe, execute, report signature) enable test automation and staged rollouts to production lines.
Validation, test cases, and common pitfalls
Validation equals repeatable tests, not one-off approvals.- Baseline test: fixed recipe on reference coupons to capture signature and nugget correlation. Repeat after electrode changes. – Drift detection: compare live signatures to baseline using simple statistical checks; don’t wait for part failure. – Fixture misalignment: often mistaken for electrical issues; verify mechanical alignment before tuning current. Avoid these mistakes: tuning current to mask poor fixturing, skipping electrode maintenance, and treating weld controllers as throwaway black boxes. Simple test cases at commissioning catch 80% of post-install failures.
Operational checklist for deploying terminology into a robotic cell
Follow these steps as you move from specification to live production.- Author a recipe template that lists every required field and unit. – Map recipe fields to PLC/weld controller tags and HMI elements. – Create deployment scripts to push recipe changes and to back up previous versions. – Define signature acceptance criteria and automate periodic validation. – Schedule electrode inspection and include that step in the maintenance pipeline. This checklist turns language into repeatable operations that teams can own and iterate on.
Performance metrics and continuous improvement
Measure what matters and keep the loop short.- Throughput tied to weld head cycle time and transformer duty. – Yield tracked per recipe revision and per electrode set. – Mean time between corrective adjustments for process drift. Use metrics to decide whether to tune recipes, change fixturing, or upgrade hardware. The goal: small, auditable changes driven by data and collaboration between controls and manufacturing engineers.
Closing synthesis
The framework shifts terminology from an informal shop-floor shorthand to a versioned, automatable specification that teams can apply across manual and robotic cells. That shared vocabulary lets us write repeatable deployment steps, validate outcomes with signatures, and keep quality predictable—work we’ve relied on when supporting large automotive lines. The result is a concise path from application-level requirements to robotic execution that operational teams adopt quickly and maintain reliably with Sunke.