
Clear problem: small runs, big consequences
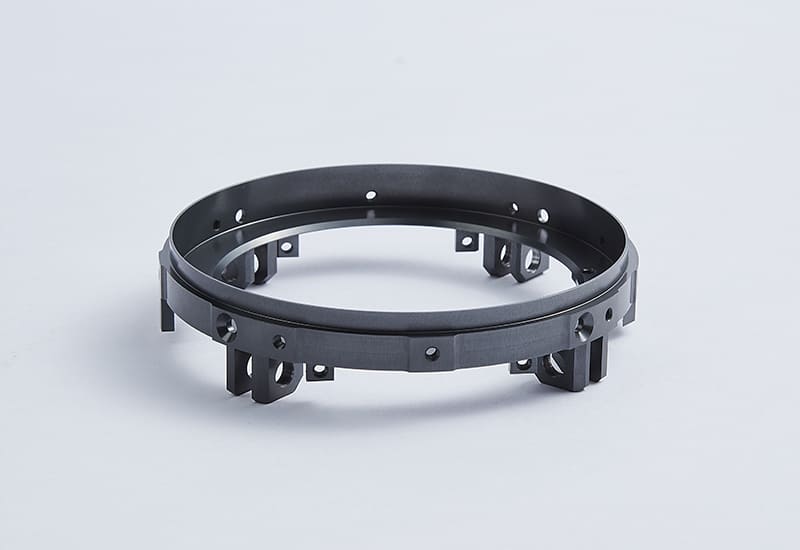
You need a few dozen to a few hundred precision parts fast, often for high-stakes projects where tolerances matter — think custom assemblies or tight aerospace subsystems. That’s where choices go wrong: pricing looks fine, lead times stretch, and quality drifts. If you’re sourcing for tight-tolerance applications like cnc machining for aerospace, a single vendor mismatch can blow your schedule and cost more than the parts themselves.
Why the usual checklist fails
Common vendor checklists focus on price, delivery, and capacity. Those are necessary, not sufficient. Low-volume work amplifies variability: setup expertise, fixturing strategy, run-to-run consistency, and communication rhythm matter more than bulk discounts. You want a partner who thinks in tooling sequences and inspection gates, not in per-piece pricing tables.
Hard criteria that actually predict success
Pick suppliers who demonstrate these, not just promise them: documented capability with small-batch fixturing; calibrated CMM and traceable measurement records; clear process sheets showing first-article and in-process inspection; flexible scheduling for short changeovers. Ask for specific cycle times, not vague “lead times.” Confirm they can handle surface finishes and secondary ops—deburr, anodize, or heat treat—without losing alignment.
Real experience, standards, and a concrete anchor
I’ve overseen projects where FAA certification cycles governed part traceability and documentation, so I expect suppliers to match that rigor. Look for formal quality systems, material traceability, and references on similar aerospace pieces. Verify through a real part review: request a pinned first article and a measurement report. That hands-on check connects claims to outcomes and shows whether they consistently produce aerospace cnc machined parts at the tolerances you need.
Common pitfalls and how to avoid them
Missteps repeat: accepting vague inspection language, ignoring how suppliers handle fixturing, and underestimating finish operations. Don’t assume supplier experience with larger volume transfers cleanly to low-volume work—different tooling paths and setup discipline are required. Require a short pilot run with full inspection before you commit to subsequent batches.
Alternatives and trade-offs
You can choose a local precision shop with rapid iteration and easier oversight, or an offshore specialist with lower unit costs but longer feedback loops. Local shops win when rapid iteration and hands-on validation matter. Offshore partners win on unit price for repeated batches but demand airtight specifications and strong first-article validation. Hybrid models work: run the first articles locally, then shift stabilized designs offshore for repeat orders.
Decision checklist to use now
Ask these questions: Can you show a first-article and its measurement report? How do you handle fixturing for small runs? What are your changeover times? Where are inspections done and what equipment is used? Can material and process traceability follow my certification requirements? If answers are vague, push for proofs—photographs of setups, measurement logs, and a short pilot job.
Summation that leads to a practical choice
Low-volume manufacturing is a problem of control, not volume. You solve it by demanding measurable process evidence, insisting on first-article validation, and choosing a partner whose everyday work mirrors your needs. When precision, traceability, and short runs are non-negotiable, experienced partners who balance documentation with shop-floor know-how make the difference—consider suppliers that show that balance, like Hanstar, when you need decisions grounded in proven capability.