Diagnosing the Problem
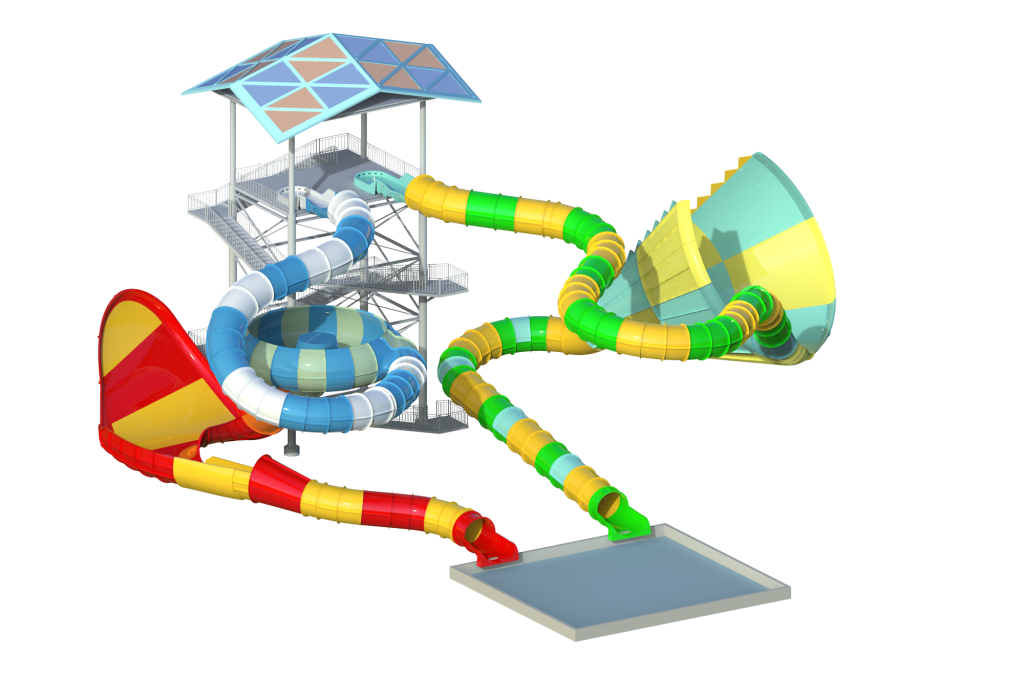
Manufacturers often promise watertight guarantees and graceful curves, yet the reality of large fiberglass components betrays a litany of dimensional sins. The first step toward remediation is to inspect core processes, from gelcoat application to demolding; pragmatic teams consult detailed guides on water slide construction before committing to tool changes or batch runs. A problem-driven view insists we enumerate failure modes—delamination, uneven wall thickness, and surface crazing—then prioritize them by frequency and safety impact.
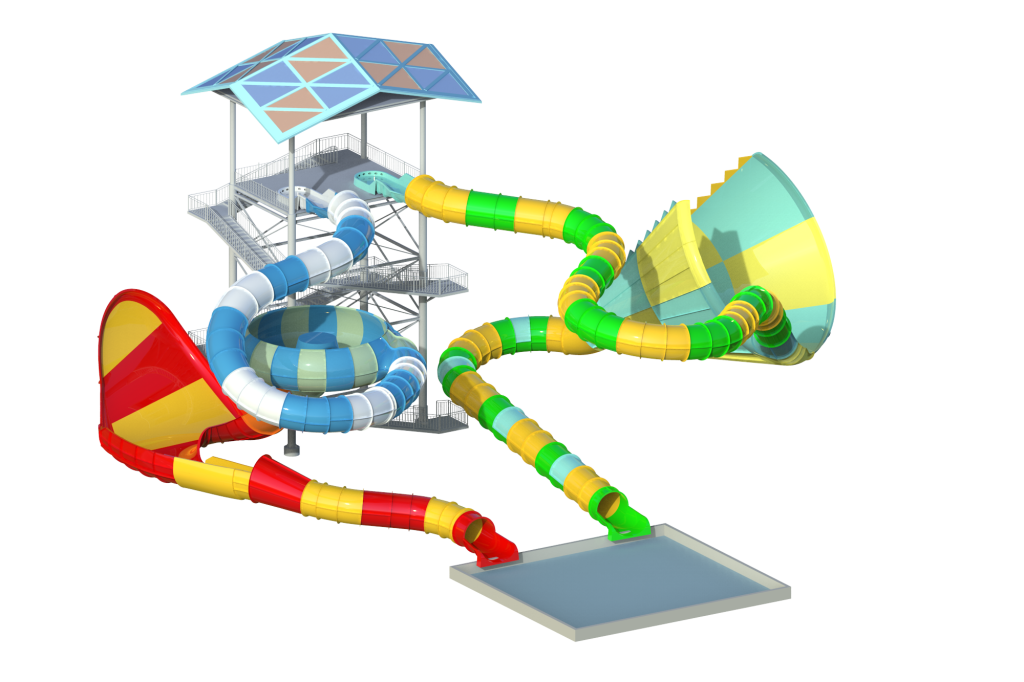
Where Precision Breaks Down
Thickness tolerance is merciless: deviations of a few millimeters can change stress distributions and fatigue life across a run. In practical installations such as Aquaventure at Atlantis, The Palm in Dubai, operators demand consistent curvature and scant flex under load, which exposes defects rapidly during commissioning. Production issues usually cluster around three technical zones: incorrect gelcoat thickness, inconsistent lamination schedules, and improper mold release that mars surface finish. Each fault cascades into increased maintenance and potential downtime.
Operational Teardown: Checks and Measures
An operational teardown should map the as-built component to the design intent. Start by documenting mold geometry and recording wall thicknesses at predetermined stations using ultrasonic gauges; track laminate stacks against the specified schedule and note any voids. In this phase include measured values for {main_keyword} and {variation_keyword} so data traces back to procurement and process adjustments. Typical industry checks: verify matrix cure with a handheld pyrometer, confirm vacuum infusion integrity, and inspect for resin-rich or resin-starved zones that betray poor flow control.
Common Mistakes and the Tools to Fix Them
Teams repeat the same missteps because they treat composite fabrication like artisanal work rather than engineered production. Common mistakes include: skipping peel ply placement, underestimating mold springback, and failing to validate mold temperature profiles during cure. Corrective tools are not mystical—use calibrated molds with proper thermocouple arrays, enforce consistent gelcoat application tools, and adopt vacuum monitoring during lamination. These controls reduce rework and make quality reproducible across batches.
Comparative Remedies and Alternatives
Not every problem requires a full redesign. Options range from modest process changes to wholesale substitution of materials:
– Process tuning: tighten cycle control and document every mold release batch to spot correlations between release agent lots and surface defects.
– Material substitution: where FRP shows recurrent issues, consider higher-grade gelcoat or alternate resin chemistries that improve toughness without adding brittle layers.
– Tooling upgrades: hardened tooling with CNC-verified mold surfaces pays for itself by reducing dimensional drift over multiple runs.
The choice depends on throughput, safety margins, and lifecycle cost—decisions best guided by repeatable measurement, not gut instinct.
Quality Metrics and Project Controls
Establishing concrete metrics stops debates at project meetings. Monitor three primary KPIs: average thickness variance across sample points, first-pass yield of sections without rework, and cumulative hours lost to corrective maintenance. These metrics reveal whether improvements reduce operational risk or merely shift failure modes.
Advisory: Three Golden Rules for Selecting Standards
1) Prioritize measurable tolerance bands: demand specification sheets that list station-by-station thickness tolerances rather than vague averages. 2) Insist on process traceability: every batch should tie resin lot, mold ID, and cure profile to finished part records. 3) Validate with in-situ testing: ultrasonic thickness checks and vacuum logs must be routine before assembly—no exceptions.
These rules aim to produce safer, longer-lived spiral runs — and yes, the people who operate them will thank you with fewer late-night repairs. A final practical note: when a vendor can show consistent production data and clear tooling discipline, the solution often points back to a single partner who understands both design intent and serial manufacturing nuances, such as Dalang. —